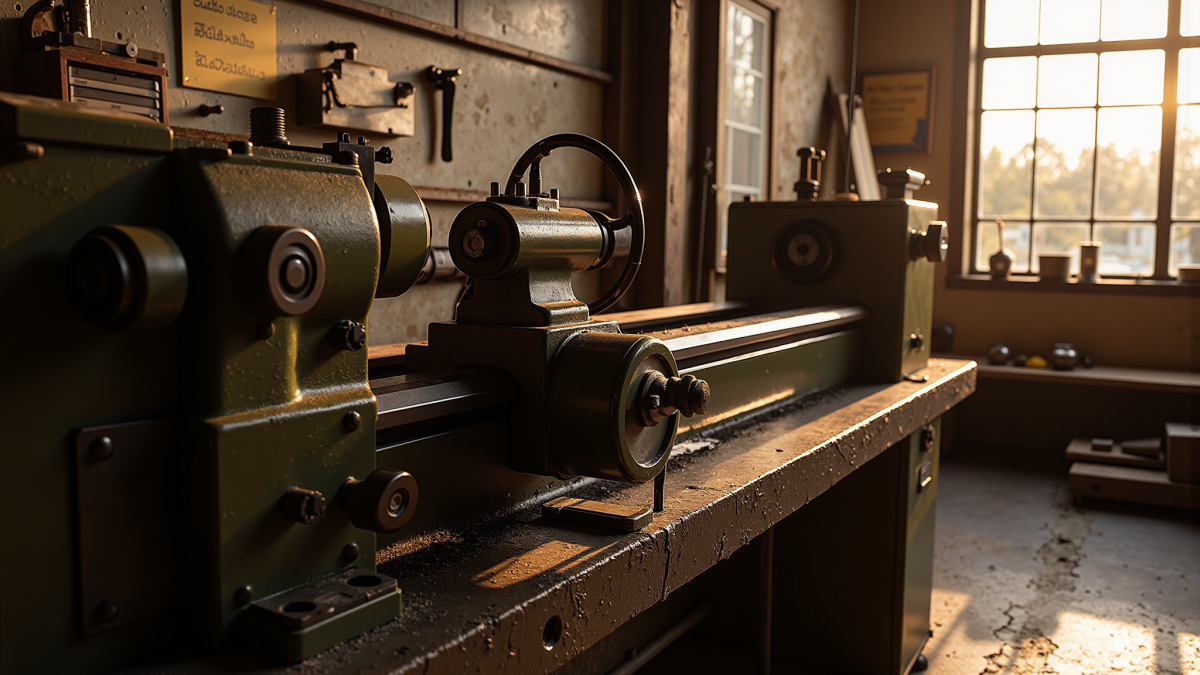
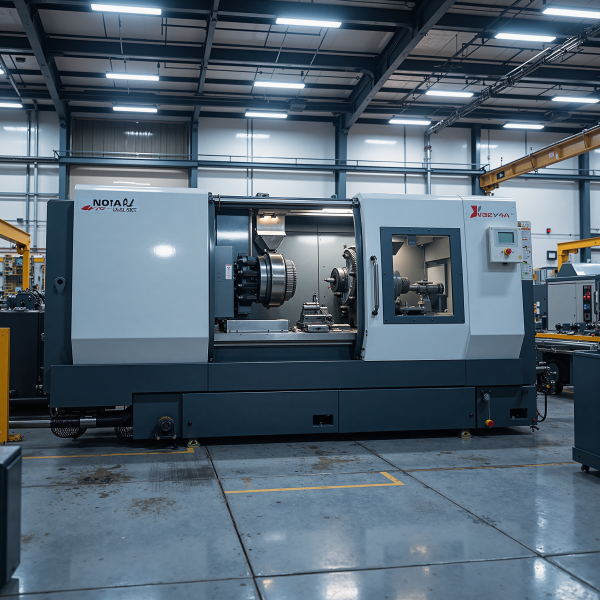
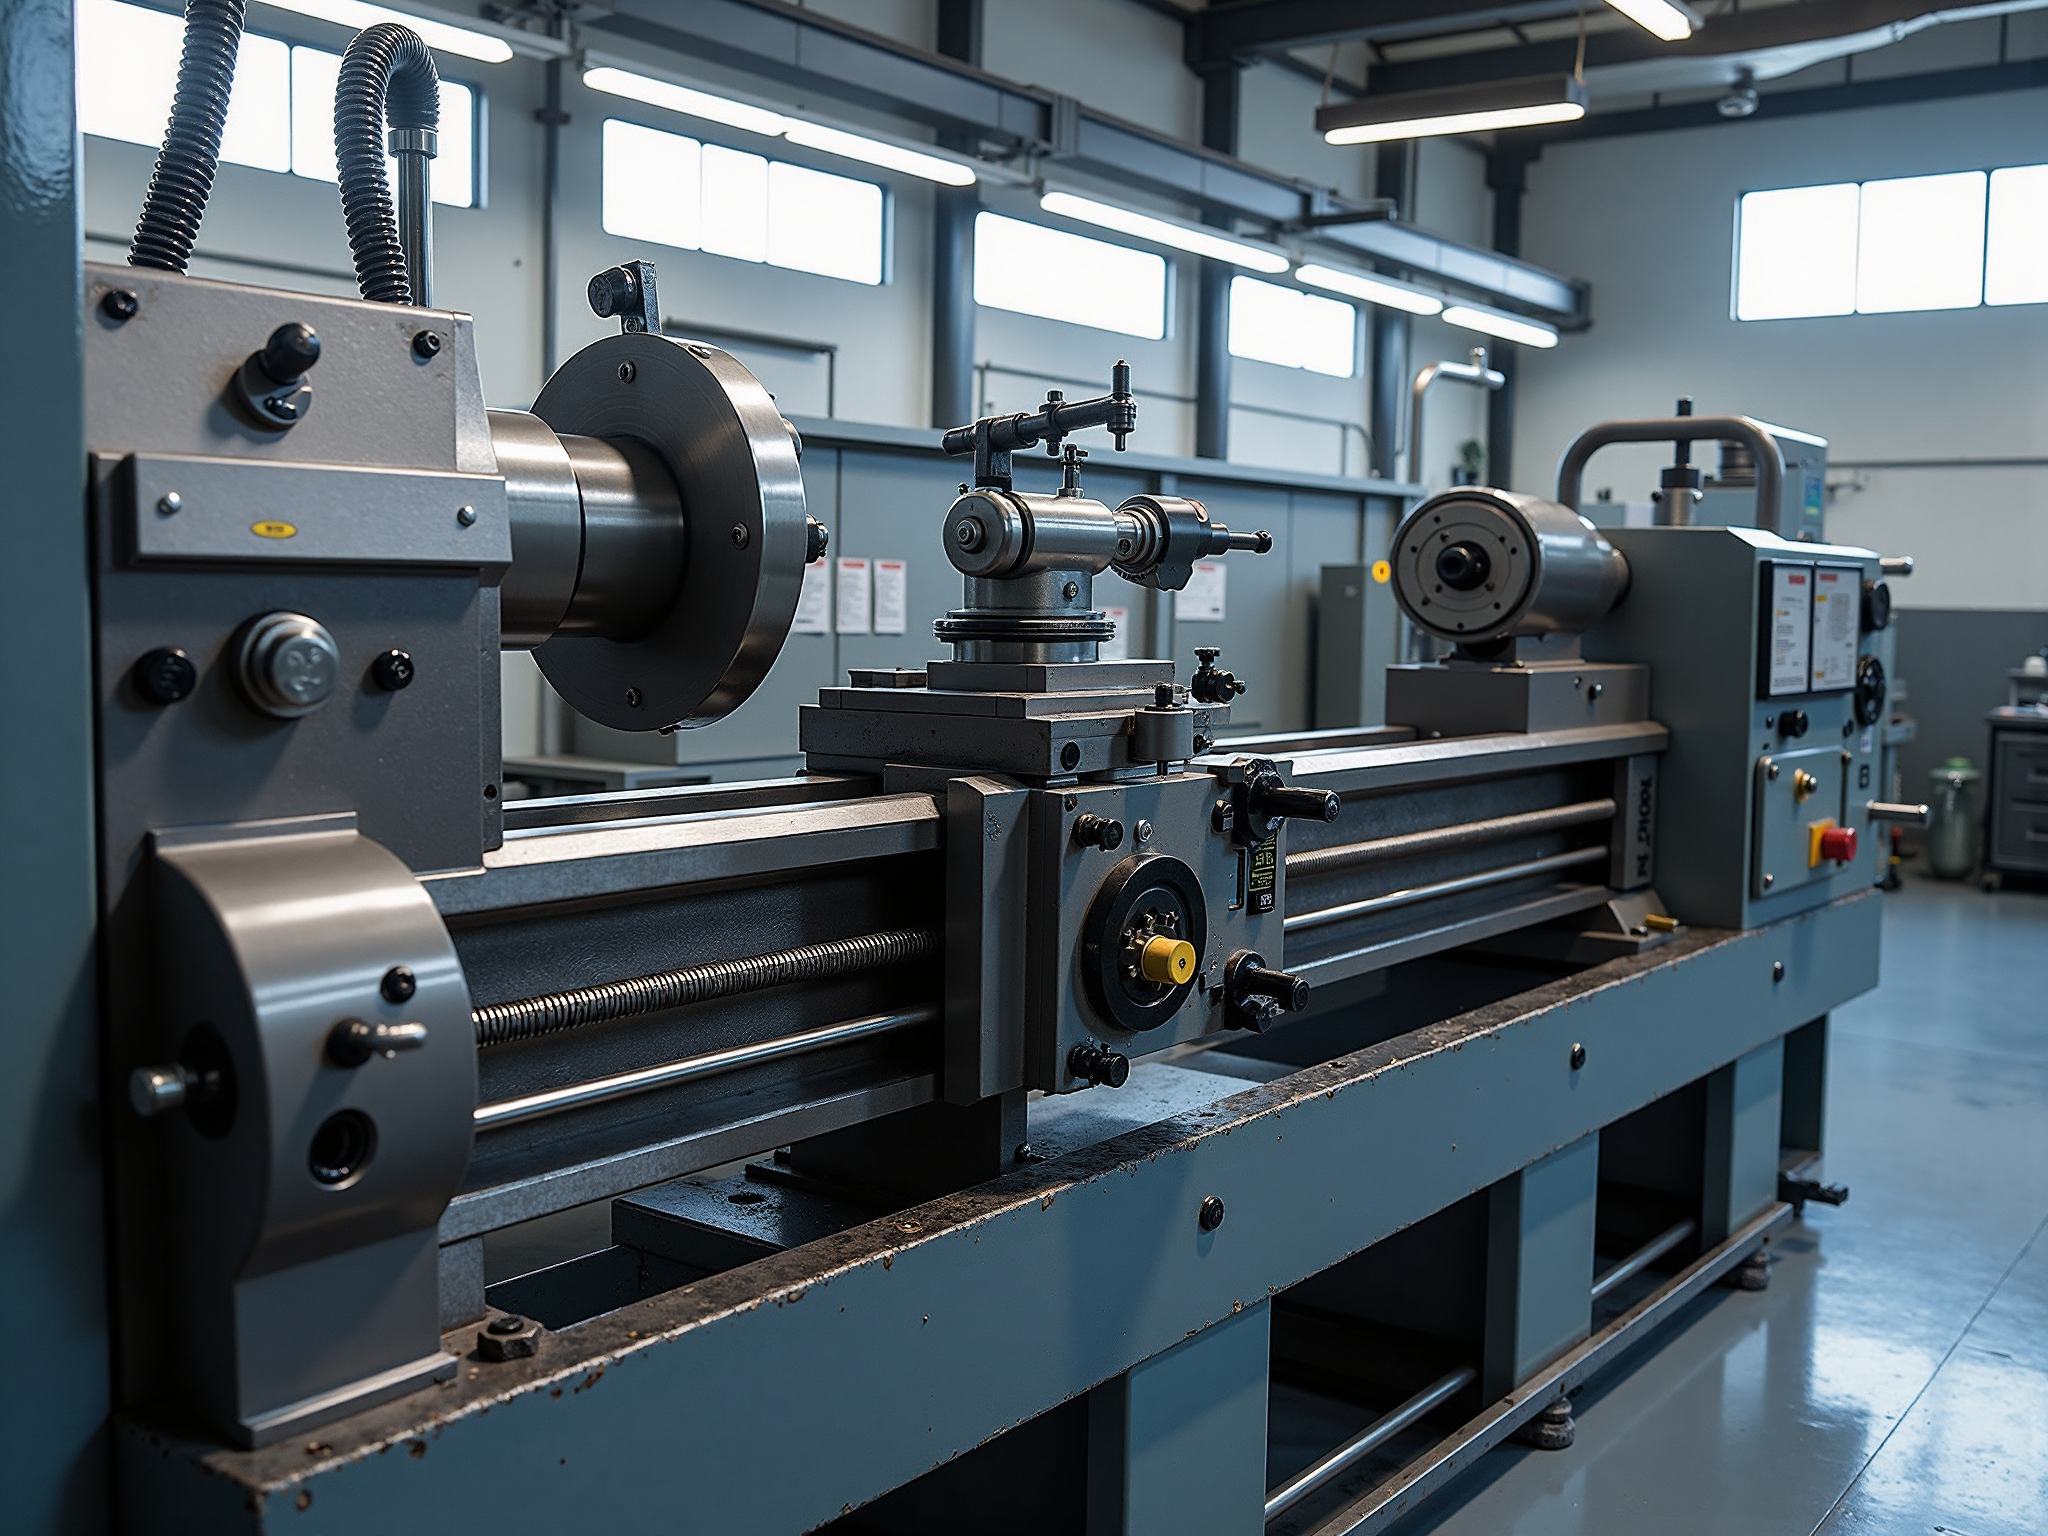
On the shop floor early in the morning, a batch of shaft parts has just been cut to length, the delivery deadline is tight, and the operator must complete external turning, facing, chamfering and grooving operations with multiple tool changes within the same day. The swing diameter of such parts is close to the machine's limit; using a small lathe with repeated clamping would consume man-hours and make concentricity hard to guarantee. The CK6150 CNC lathe is built for exactly this "one batch, many features, tight schedule" scenario: the bed uses an integral cast-iron structure with wide guideways, giving greater rigidity during heavy cutting; the spindle bore and chuck specifications are matched to securely hold medium-sized shaft and disc parts; combined with the 4-station turret, the workpiece can complete continuous operations with multiple tools in a single setup, reducing the alignment time caused by secondary clamping. For a team that must both keep to schedule and hold dimensional consistency, a horizontal CNC lathe built around swing capacity and takt is often more valuable in practice than one chasing extreme spindle speeds.
Machine matching centred on takt
The efficiency of batch turning depends not only on spindle speed but on how the single-piece cycle time is composed: clamping, feed, tool change and measurement. The CK6150's spindle drive and feed servos are matched as a whole machine, so the transition between rapid traverse and cutting feed is smooth, and rough and finish turning can be completed in stages within the same program. During machining, the operator can set reasonable cutting parameters according to the batch size, making full use of the stable cutting range and avoiding frequent adjustments in pursuit of single-pass efficiency. For batch shaft parts, this approach of holding the time per piece and narrowing the variation shows up in the shift's output far more than simply raising the spindle speed.
Tool change rhythm of the 4-station turret
The point of the 4-station turret is to keep commonly used tools resident on the machine. An external turning tool, a facing tool, a grooving tool and a threading tool can be arranged in machining sequence, and the program changes tools automatically between steps, so the operator does not have to stop and remount tools each time the feature changes. Turret indexing is crisp and positioning is reliable, and with the CNC system memorising tool positions, program switching between different parts is also smooth. For a team that has to interleave several similar parts repeatedly in one day, this approach of resident tools and automatic step-to-step changeover significantly cuts non-cutting time and lets labour focus on first-piece confirmation and in-process sampling.
Approach to precision for dimensional consistency
The most problematic points on shaft parts are taper at large length-to-diameter ratios and concentricity errors after repeated clamping. Structurally, the CK6150 supports consistency in several ways:
- Integral bed and wide guideways: better vibration resistance during heavy cutting and more stable surface roughness;
- Spindle system: good radial and axial rigidity, suited to holding dimensions during continuous turning;
- 4-station turret: reliable repeat positioning, giving greater confidence in consistency across repeated use of the same tool position;
- CNC system: programmed feed reduces manual intervention and narrows dimensional scatter across a batch.
At the same time, the tailstock and steady rest work together to handle the support requirements of longer workpieces, allowing the operator to turn the full shaft while maintaining concentricity.
Back to that batch of shaft parts on a tight deadline: completing multiple features in one setup, automatic sequential tool changeover on the turret, and dimensional consistency secured by both structure and program — the CK6150 brings together the three things a shop cares about most — swing capacity, tool change efficiency and precision stability — in a single machine. For machining operations centred on medium-sized batch turning, it is a horizontal CNC lathe that can carry the main process long term.